Home >What We Do > Quality And Acceptance Standards For Conventional Metal Injection Molding Parts
Mold Making & Powder‑Metallurgy Manufacturing Expert Specializing in Metal Injection Molding, DFM for sintered components, quality‑control systems and custom MIM manufacturing solutions.
Table of Contents
In the article “Common Metal MIM Defects, Causes and Solutions”, we mentioned that product designers and procurement buyers need a thorough understanding of typical MIM part defects. This knowledge supports clear quality evaluation after placing orders with MIM manufacturers. Since every project has unique geometry, cosmetic expectations and functional requirements, buyers should define project‑specific MIM acceptance criteria.
This article cannot cover custom quality rules for every individual component. However, it delivers practical reference acceptance guidelines for conventional sintered MIM parts, aligned with widely‑recognized MPIF‑35 MIM industry specifications.
The quality standards for MIM parts mainly refer to MPIF Standard 35 (Metal Powder Industries Federation powder metallurgy standard of the United States) and ASTM B883 (standard for metal injection molded materials). The corresponding Chinese national standard is GB/T 26726 (standard for metal injection molded materials).
MPIF Standard 35 classifies MIM materials into several standard grades based on density classes. Each grade specifies chemical composition, density, mechanical properties and reference hardness. Taking MIM-316L as an example, the standard requires density ≥7.5g/cm³ (95% theoretical density), tensile strength ≥450MPa, elongation ≥40%, and hardness HRB45-80.
ISO 22068 (international MIM standard) is basically equivalent to MPIF Standard 35. The difference is that ISO 22068 adds mandatory requirements for debinding process verification and sintering furnace temperature uniformity (TUS).
| Test Item | Test Method | Frequency | Acceptance Standard | Impact of Non-Conformity |
|---|---|---|---|---|
| Sintered Density | Archimedes water immersion method (ASTM B962) | 3–5 pieces per sinter batch | ≥96% theoretical density (316L ≥7.5g/cm³) | Degraded mechanical performance / leakage |
| Dimensional Tolerance | CMM / optical comparator | First article + sampling 5 pieces every 2 hours | Dimension ±0.3–0.5% / Cpk≥1.33 | Assembly issues |
| Carbon Content | Carbon-sulfur analyzer (LECO) | Once per batch | 316L ≤0.03% /17-4PH ≤0.07% | Reduced corrosion resistance |
| Metallographic Structure | Metallographic microscope (ASTM E3) | 2 pieces per batch | Porosity ≤2% / grain size ≥Grade 5 | Substandard overall performance |
| Mechanical Properties | Universal testing machine (ASTM E8) | 3 pieces per batch | In accordance with corresponding grades in MPIF 35 | Unqualified service performance |
| Surface Roughness | Roughness tester | 5 pieces per batch | Ra 0.8–1.6μm (as-sintered) | Unqualified appearance / functional surfaces |
| Hardness | Rockwell / Vickers hardness tester | 3–5 pieces per batch | In accordance with corresponding grades in MPIF 35 | Substandard wear resistance / strength |
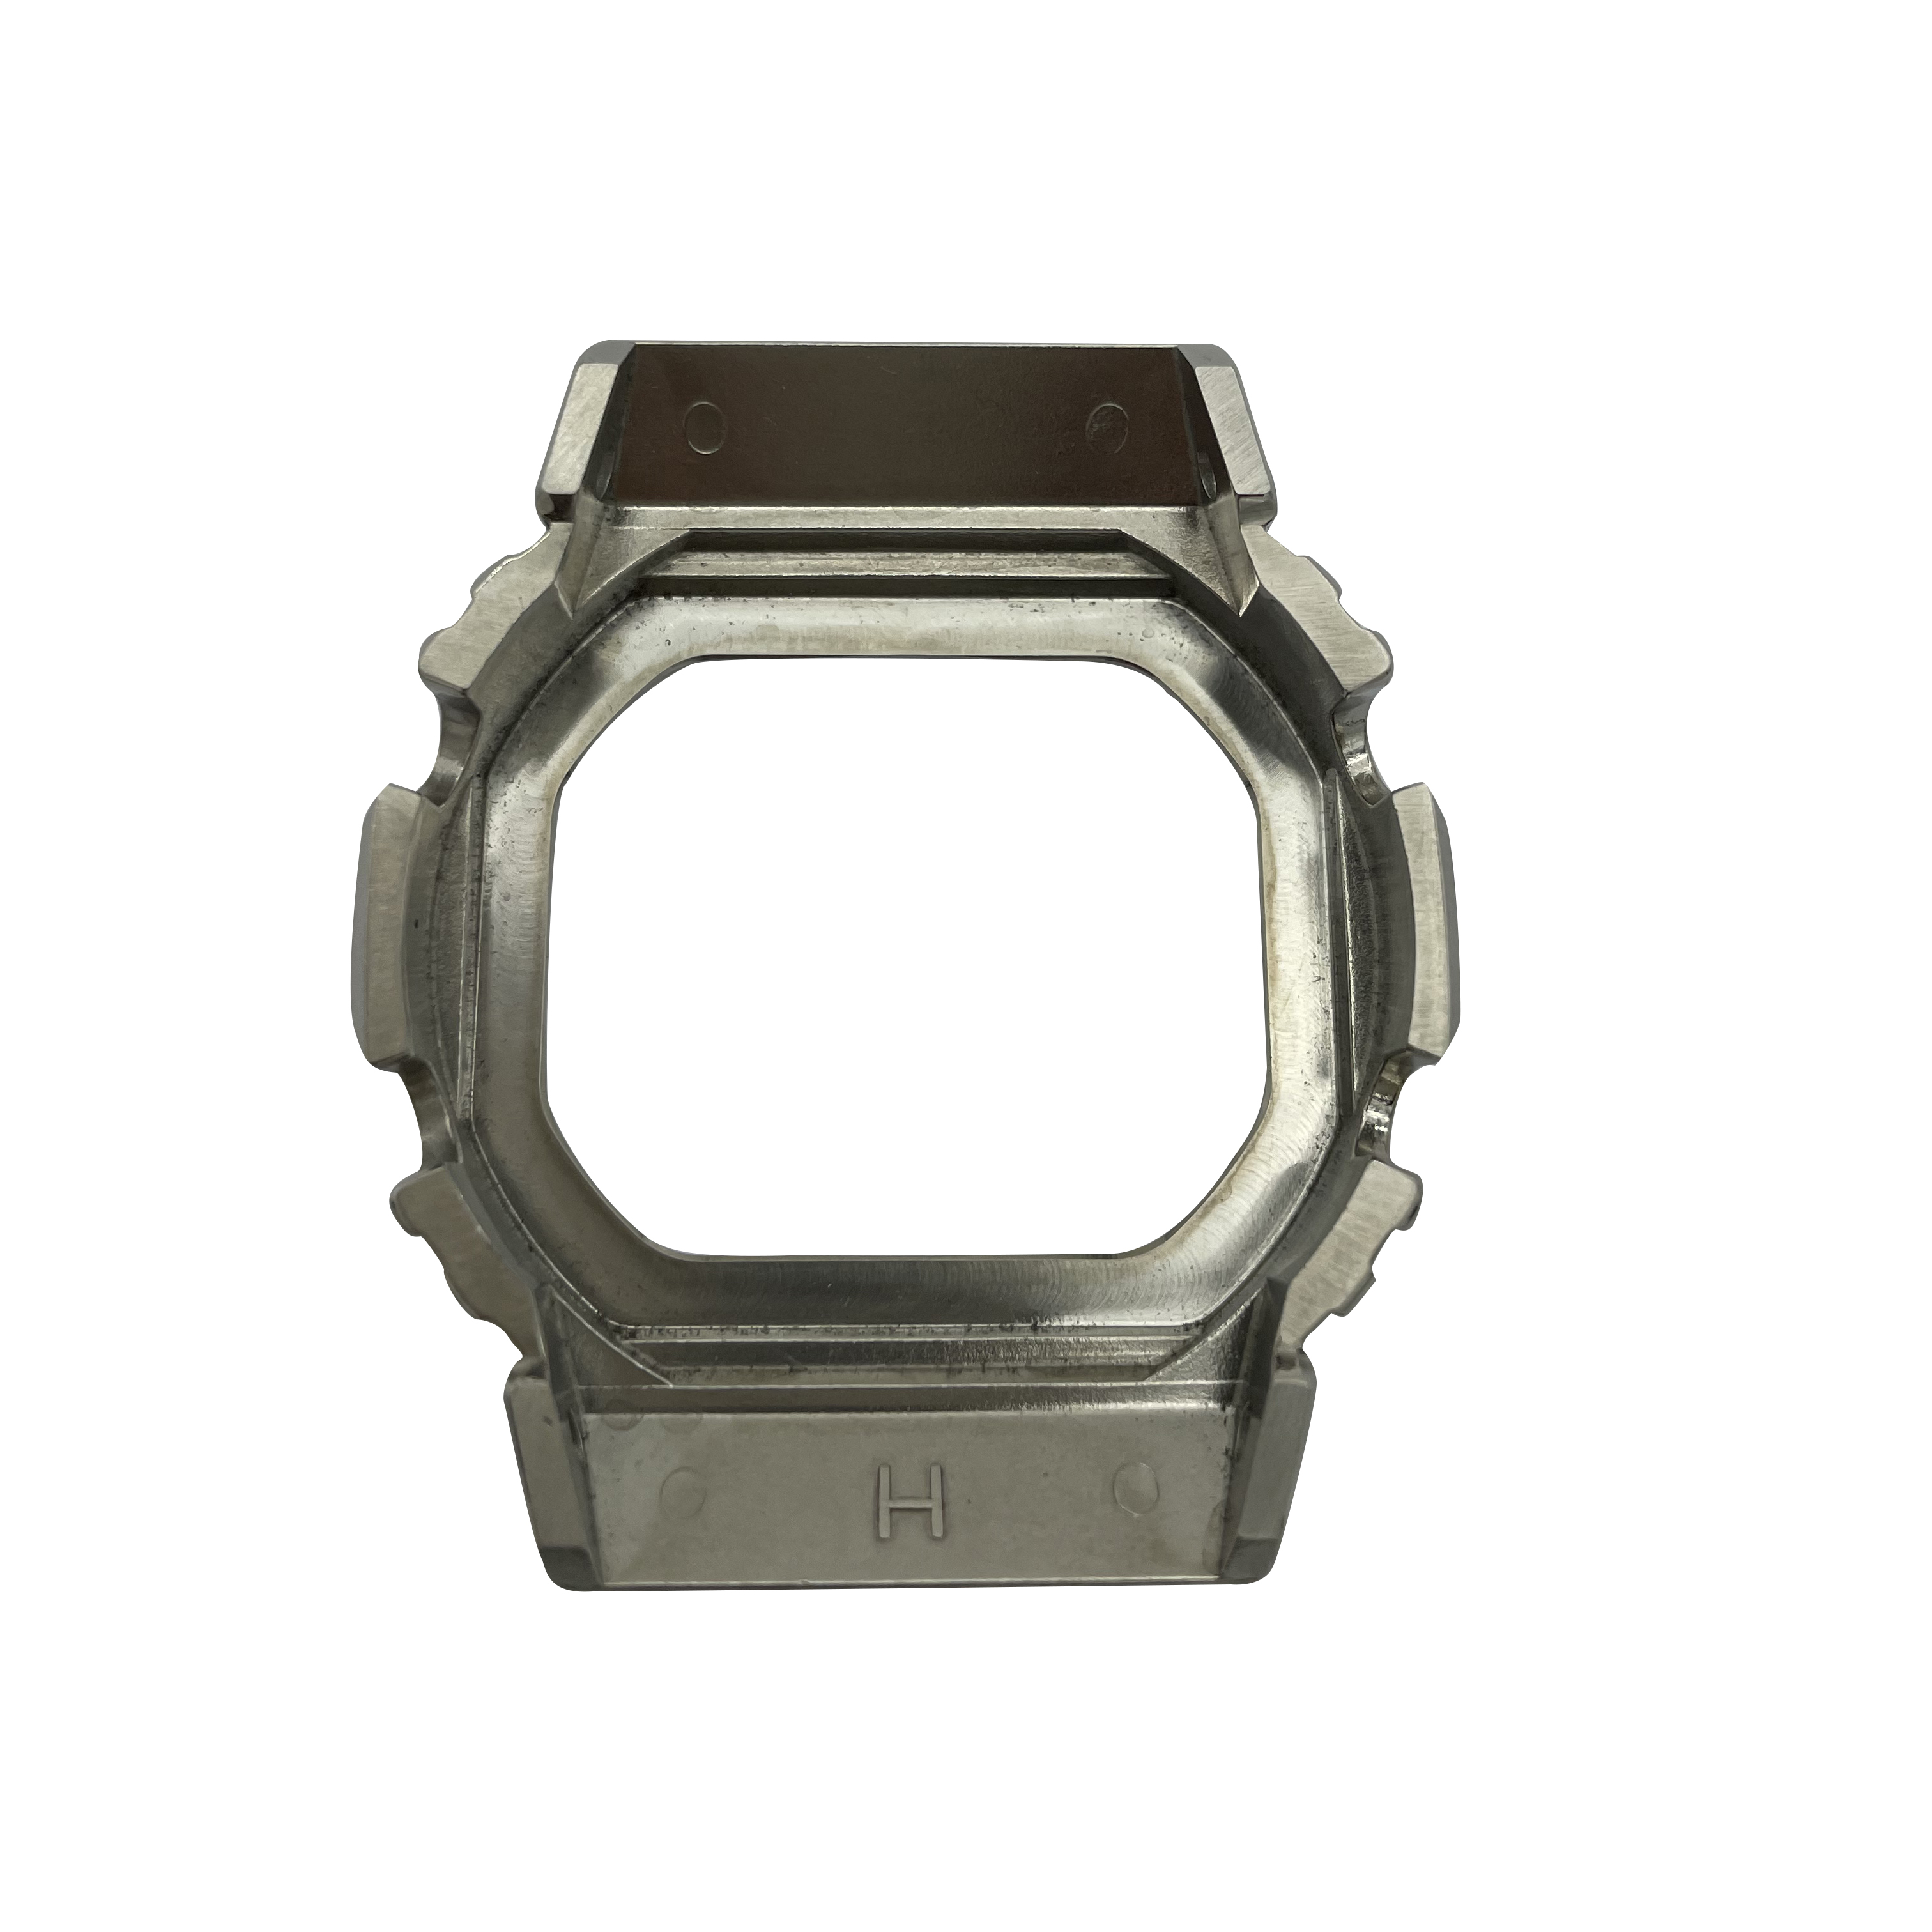
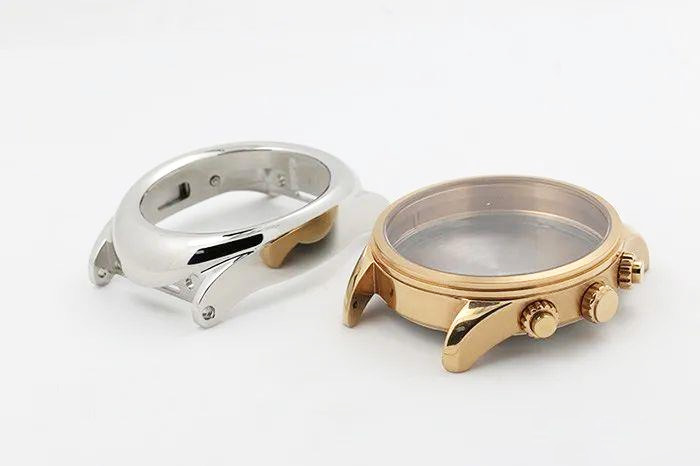
Class A surfaces represent the highest cosmetic requirements. These surfaces are directly visible under normal end‑use conditions, such as exposed housing surfaces for consumer‑electronic MIM hardware. For Class‑A MIM surfaces, both visual smoothness and functional performance are critical. Minor sinter discoloration, gate vestiges and scratches must be tightly controlled. Cosmetic‑grade post‑finishing such as electropolishing or tumbling is often required to meet Class‑A visual benchmarks.
Class B surfaces are exposed but not prominently visible in daily operation, for instance the side or bottom face of assembled components. They can be seen during disassembly but are not the primary focus of observation. Moderate, non‑distracting surface imperfections are permissible as long as assembly performance remains unaffected.
Class‑C surfaces include internal structural faces, hidden mating contact surfaces, setter‑contact sintering areas and non‑visible inner cavities. Functional performance takes priority over visual appearance. Minor surface marks are acceptable provided they do not impair assembly, wear performance or corrosion resistance.
This set of reference standards applies under the precondition that component functionality remains unimpaired. It serves for visual comparison and shall not override project‑specific drawing requirements or official industry specifications such as MPIF‑35.
Standard visual inspection shall first be performed at 30 cm distance for 3‑5 seconds. If suspected defects are spotted, the inspector moves to 50 cm and observes for 3‑7 seconds. Imperfections that become faint or hardly visible at 50 cm are regarded as acceptable.
Visual assessment shall take place under standard factory fluorescent lighting, performed by inspectors with corrected visual acuity ≥0.7.
Two main observation angles shall be applied: perpendicular to the target surface, and 45‑degree oblique view from above or below.
Note: Visual check alone cannot detect subsurface micro‑cracks or internal porosity. Critical high‑load MIM parts require supplementary metallographic sectioning, X‑ray or mechanical‑property sampling inspection.
Zero flash tolerance applies for moving‑part mating holes, pin interfaces and sliding friction surfaces. Minor flash on hidden bosses and internal structures is allowed only if it does not interfere with assembly or movement. Exposed outer surfaces must be smooth to touch without sharp burrs that risk scratching operators or mating components.
For flat housing‑type MIM parts resting on a reference flat plate, overall warpage shall not exceed 0.3 mm. For other structural components, slight sinter‑induced deformation is acceptable as long as fit‑check with mating parts passes and functional performance stays intact. Severe warpage will trigger rejection, as it changes assembly clearance and may introduce unexpected stress.
As‑sintered MIM dimensions follow percentage‑based tolerance rules. Tighter precision can be achieved by secondary CNC sizing for critical mating features. The table below offers general reference dimension tolerances for as‑sintered MIM parts.
表格
| Dimension Range (mm) | As‑Sintered Reference Tolerance (mm) |
|---|---|
| 0 – 10 | ±0.05 |
| 10.1 – 50 | ±0.10 |
| 50.1 – 100 | ±0.15 |
| 100.1 – 200 | ±0.20 |
| Over 200 | ±0.25 |
表格
| Defect Type | Class A | Class B | Class C |
|---|---|---|---|
| Surface / Sub‑Surface Cracks | Not allowed | Not allowed | Not allowed for load‑bearing zones; minor non‑stress‑area surface scratches permitted if no impact on function |
| Short Shot (Incomplete filling) | Not allowed | Not allowed | Minor localized imperfection acceptable only if it does not affect assembly or mechanical performance |
| Sinter Flow Marks / Sinter Streaks | Shall meet pre‑approved engineering sample benchmark | Shall meet pre‑approved engineering sample benchmark | Shall meet pre‑approved engineering sample benchmark |
| Sink Marks / Sinter Sags | No visible or tactile depressions under 45°‑90° viewing angle | No visible or tactile depressions under 45°‑90° viewing angle | No visible or tactile depressions that interfere with assembly |
| Dark Spots / Sinter Discoloration / Stains | Max 2 spots, spacing >100 mm, each spot area <0.4 mm² | Max 3 spots, spacing >100 mm, each spot area <0.5 mm² | Max 4 spots, spacing >100 mm, each spot area <0.9 mm² |
| Scratches / Handling Impacts | Each scratch ≤8 mm long, ≤0.05 mm wide | Each scratch ≤10 mm long, ≤0.10 mm wide | Each scratch ≤25 mm long, ≤0.15 mm wide |
| Gate Vestige Marks | Not allowed to protrude; must be flush or post‑processed smooth for exposed cosmetic surfaces | Gate residue ≤0.3 mm protrusion, no sharp edges | Gate vestige ≤0.8 mm protrusion, no functional interference |
Exposed cosmetic Class‑A surfaces must have flush gate positions. Gate remnants shall be removed by tumbling, grinding or electropolishing to eliminate sharp edges that cause scratching.
For unexposed mating Class‑B surfaces, gate‑vestige protrusion must be controlled within 0.3 mm and shall not interfere with part assembly.
On hidden Class‑C internal features with no cosmetic or assembly constraints, gate‑break natural fracture is acceptable with maximum protrusion limited to 0.8 mm.
Density check: General structural MIM components require sintered relative density ≥95‑96%. High‑fatigue applications need HIP treatment to raise density above 99 %.
Porosity: Open interconnected surface porosity must be documented for parts requiring plating; high‑density pre‑condition is mandatory before electroplating to avoid blistering.
Heat‑treatment validation: Precipitation‑hardening grades like 17‑4PH must pass hardness sampling inspection to verify proper aging.
Many buyers only reference plastic‑injection‑molding acceptance standards for MIM sintered metal parts, overlooking MIM‑specific risks including sinter discoloration, porosity, gate‑vestige residual and sinter warpage. This mismatch creates endless sample‑re‑work and batch‑quality disputes. Send your drawings, surface‑classification rules and acceptance thresholds to Harbermetal. Our QA and engineering team will define reasonable MIM‑oriented acceptance benchmarks at the pre‑tooling DFM phase, avoiding post‑mass‑production quality conflicts.
Harber Industrial Limited (brand Harbermetal) is an ISO‑certified full‑chain China‑based MIM manufacturer rather than a trading intermediary. We maintain complete in‑house workflows covering feedstock qualification, mold development, metal injection molding, multi‑stage debinding, controlled‑atmosphere / vacuum sintering, dedicated heat‑treatment, secondary‑CNC sizing and multiple surface‑finishing options.
Our QA department establishes project‑tailored acceptance standards aligned with MPIF‑35 MIM reference specifications before sampling starts. We classify Class A/B/C surfaces together with customers, clarify visual‑defect limits, density requirements, hardness thresholds and sampling‑inspection schemes. Our in‑house lab supports CMM dimension measurement, density testing, hardness testing, metallographic analysis and salt‑spray corrosion validation. We deliver First‑Article‑Inspection reports, batch‑lot traceability documents and complete test records for automotive hardware, power‑tool assemblies, lock‑system components, consumer‑electronics and non‑implant medical‑auxiliary MIM projects, for both prototype sampling and medium‑to‑high‑volume serial‑production.
Contact information
Email: sales@harber‑mim.com
Tel: +86 0769‑82389116
In real‑world procurement scenarios, complete acceptance specifications for MIM sintered metal parts are far more comprehensive than these reference guidelines. They can cover packaging requirements, labeling rules, surface‑finishing benchmarks, metallurgical indicators, mechanical‑property thresholds, assembly‑fit validation and environmental‑reliability testing.
Plastic‑injection‑molding acceptance rules cannot be directly copied over for sintered MIM metal components. Buyers shall formulate detailed project‑specific acceptance criteria based on actual service conditions. Cooperate with a full‑service MIM manufacturer such as Harbermetal to confirm all acceptance rules before mold investment, ensuring finished sintered components satisfy both visual expectations and core functional requirements.
Ready to define acceptance standards for your custom MIM project? Submit your drawings and functional specifications for a free DFM manufacturability assessment and transparent quotation.
Request A Free Quote
The most commonly used method is the Archimedes water immersion method (ASTM B962), with precision up to ±0.01g/cm³. The metallographic method (area percentage method for porosity) is used to assist in analyzing the uniformity of density distribution. Density is the core quality indicator of MIM parts, and ≥96% of the theoretical density is regarded as qualified.
The tolerance of as-sintered dimensions is ±0.3–0.5%. After sizing, it can reach ±0.1–0.3%. A process capability Cpk ≥1.33 is considered acceptable. Dimensional consistency is controlled by three major factors: temperature uniformity of the sintering furnace (TUS ≤ ±5℃), feedstock consistency (MI fluctuation ≤10%), and stability of injection parameters.
316L requires carbon content ≤0.03% (ultra-low carbon grade), while 17-4PH requires ≤0.07%. Excessive carbon content will precipitate carbides and trigger intergranular corrosion. The key to carbon content control lies in the residual binder rate of the debinding process (target ≤0.5%) and the purity of the sintering atmosphere (H₂ ≥99.99%).
International standards include MPIF Standard 35 and ASTM B883, and the Chinese national standard is GB/T 26726. MIM parts for medical devices also need to comply with the ISO 13485 system and ISO 10993 biocompatibility standards.
Low sintered density (caused by insufficient sintering temperature or holding time), out-of-tolerance dimensions (caused by uneven furnace temperature or inconsistent feedstock batches), excessive carbon content (incomplete debinding or atmospheric contamination), surface porosity (sintering pores exposed after polishing), and deformation (improper loading setup or gravity-induced distortion).
 Send A Message
If you are interested in our products and want to know more details,please leave a message here,we will reply you as soon as we can.